Premium selection of custom manufactured bags combining thermal performance, style, and extreme durability.

Understanding the macroeconomic forces, market trends, and supply chain shifts in the thermal insulation bag industry.
The global insulated cooler bag market is witnessing unprecedented growth, driven by changes in consumer lifestyle, expanding cold chain logistics networks, and the boom in on-demand food delivery platforms. No longer just a leisure item for picnics, soft cooler bags have become vital components in commercial transport, biomedical logistics, and retail grocery distribution.
As governments worldwide implement strict single-use plastic bans, industries are transitioning toward highly reusable, multi-layered thermal bags. This structural shift has positioned China as the leading manufacturing hub, offering advanced fabric technology, RF welding, and comprehensive OEM/ODM supply chains that guarantee high thermal efficiency at competitive scale.
Furthermore, the consumer division of this industry demands aesthetic appeal combined with professional-grade function. Outdoor and lifestyle brands require durable finishes (like 500D TPU and heavy-duty PVC), leakproof zippers, and lightweight materials. Sourcing directly from certified Chinese manufacturers allows international buyers to leverage raw material ecosystems, keeping acquisition costs low while keeping quality standards high.
The global thermal bag market is growing at a compound annual growth rate (CAGR) of over 6.8%. Increasing demands for fresh meal preps and organic grocery transport are primary drivers.
Over 75% of top-tier global brands now require eco-friendly alternatives including RPET fabrics, biodegradable TPU liners, and PFAS-free water repellent coatings.
Ensuring temperature integrity for last-mile pharmaceutical distribution and gourmet food delivery has shifted the engineering focus to high-density foam and airtight zipper designs.
The technical architecture behind professional-grade soft-sided cooler bags and temperature retention parameters.
Thermal performance starts with the core. Most standard consumer bags use basic 2-3mm EPE (Expanded Polyethylene) foam. Our commercial-grade coolers use high-density NBR (Nitrile Rubber) closed-cell foam or thick PU (Polyurethane) foam, ranging from 15mm to 30mm. This complex structure exhibits low thermal conductivity, drastically slowing heat transfer.
Stitched seams create tiny needle holes that leak liquid and allow air exchange, which diminishes ice life. We utilize High-Frequency Radio Frequency (RF) Welding technology to fuse TPU-coated fabrics together, creating permanent, molecular-level waterproof bonds that are completely leakproof and airtight.
To withstand rough outdoor exposure and transport environments, our bags are made with 500D to 840D TPU-laminated Nylon or heavy-duty PVC. These materials are puncture-resistant, UV-resistant, and chemically stable, protecting the inner foam structure from compression and environmental degradation.
The interior liner uses food-safe PEVA or TPU film. Unlike cheap PVC alternatives, TPU film contains no harmful plasticizers, does not crack at freezing temperatures (-30°C), and prevents mold and bacterial growth, meeting FDA and LFGB compliance requirements.
| Material Tier | Core Insulation Layer | Outer Fabric | Liner Material | Average Ice Retention |
|---|---|---|---|---|
| Industrial / Professional | 25mm Closed-Cell NBR/PVC Foam | 840D Nylon TPU Double-Laminated | FDA Food-Safe TPU Film (Seamless) | 48 - 72 Hours |
| Commercial / Delivery | 15-20mm High-Density PU Foam | 500D PVC Tarpaulin (Waterproof) | Thick PEVA (RF Welded) | 24 - 36 Hours |
| Retail / Promotional | 5-10mm EPE Foam | 600D Polyester (Water-repellent) | Seamless PEVA Lining | 6 - 12 Hours |
Engineered thermal systems optimized for specialized commercial, recreational, and industrial use cases.
Strict temperature controls are required to transport vaccines, insulin, biological samples, and laboratory reagents. Our industrial-grade medical cooler bags integrate specialized slots for gel ice packs and digital temperature displays, securing an uninterrupted cold chain between 2°C and 8°C.
For catering services and meal-delivery platforms (like UberEats and Deliveroo), temperature retention directly dictates food safety and customer satisfaction. We design large-capacity thermal backpacks featuring inner dividers, moisture-wicking vents, and heat-reflective foil linings.
Designed for fishing, marine excursions, and long off-road trips. These bags feature ultra-durable, thick outer skins, chemical-resistant hardware, and high ultraviolet protection factor (UPF) finishes to withstand continuous saltwater spray and harsh sun exposure without cracking.
Learn more about Hebei Ripped Fashion Co., Ltd. and our end-to-end industrial quality management workflow.
Company Profile
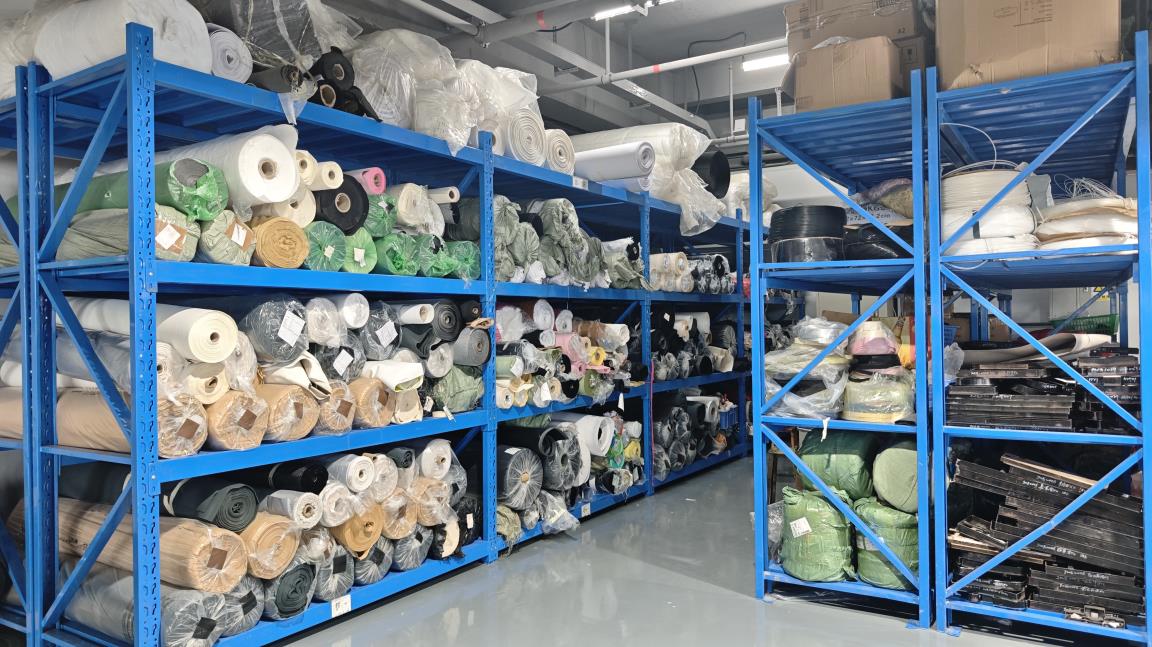
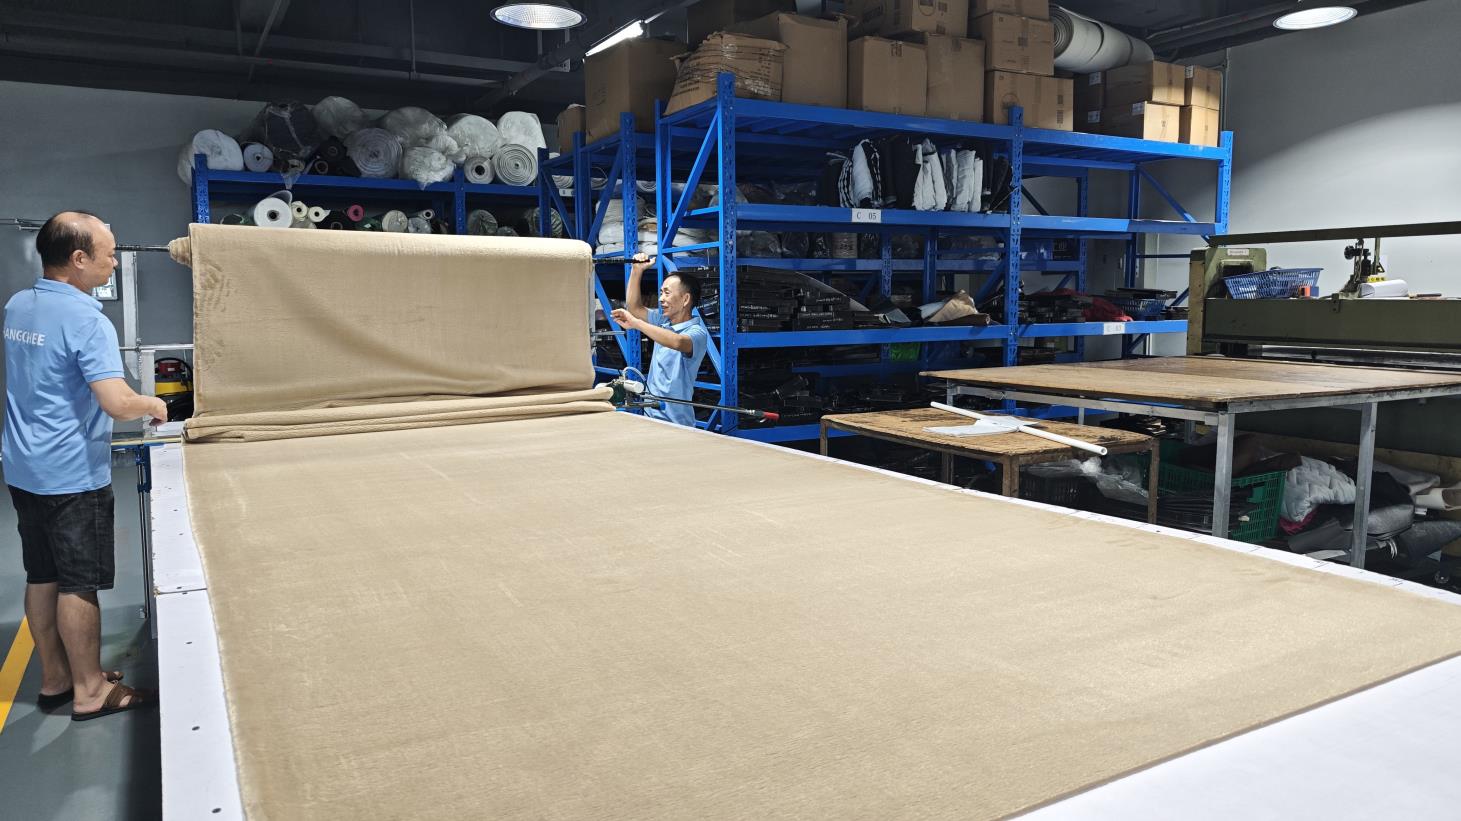
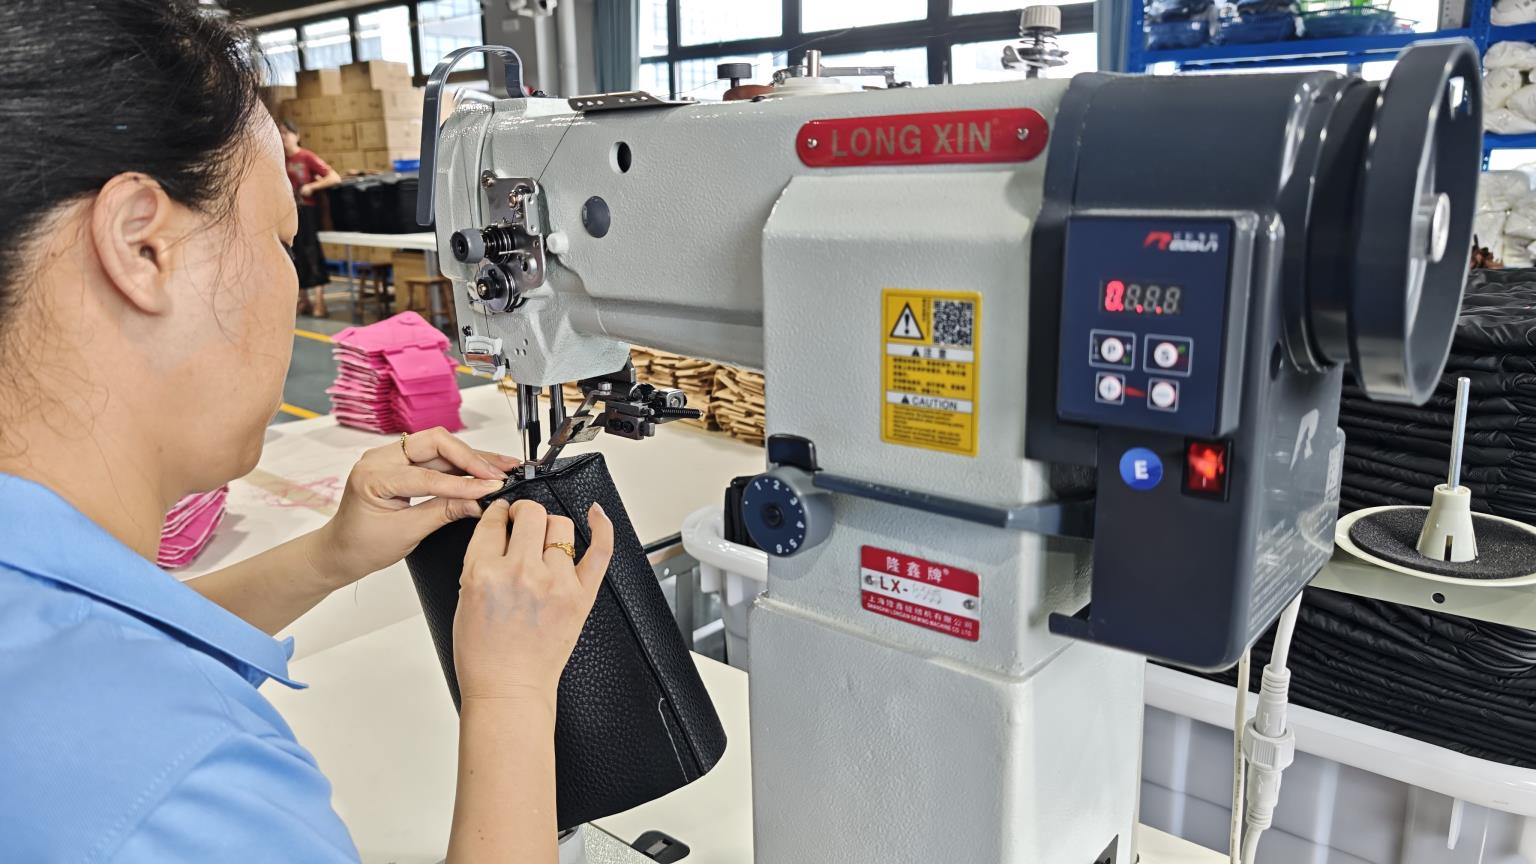
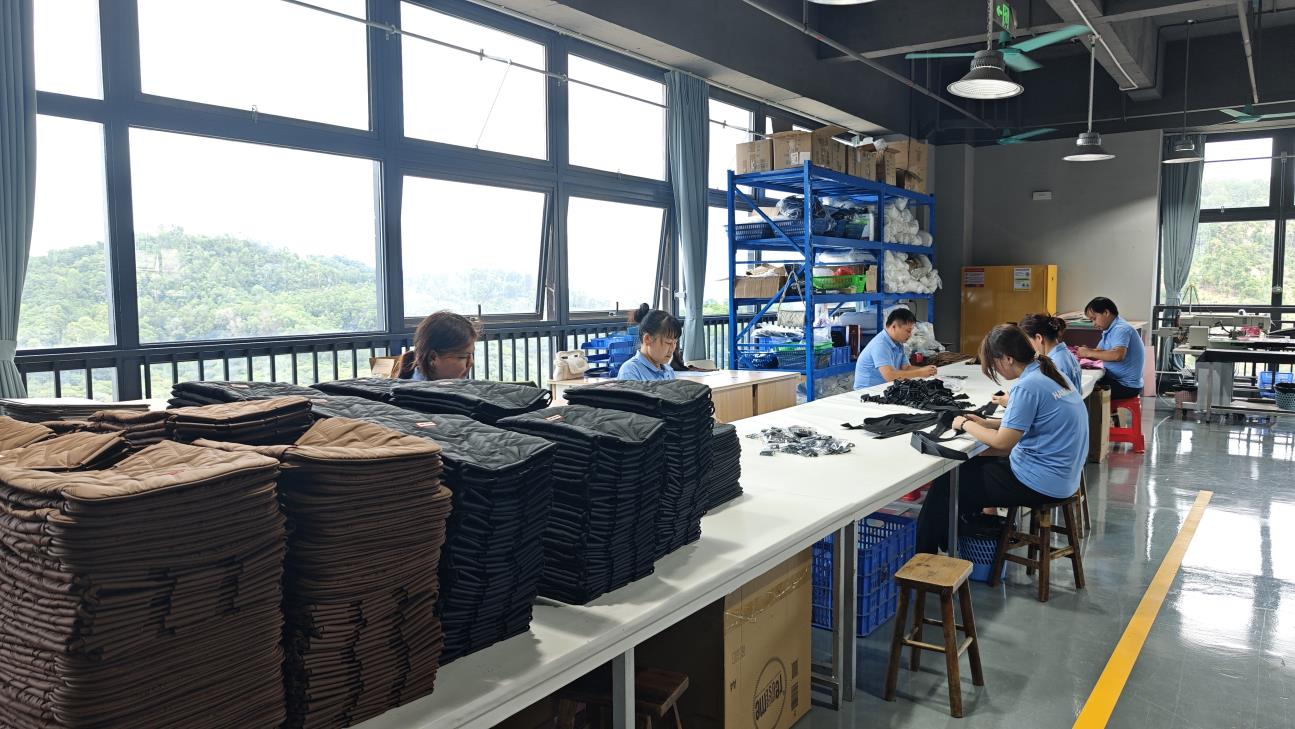
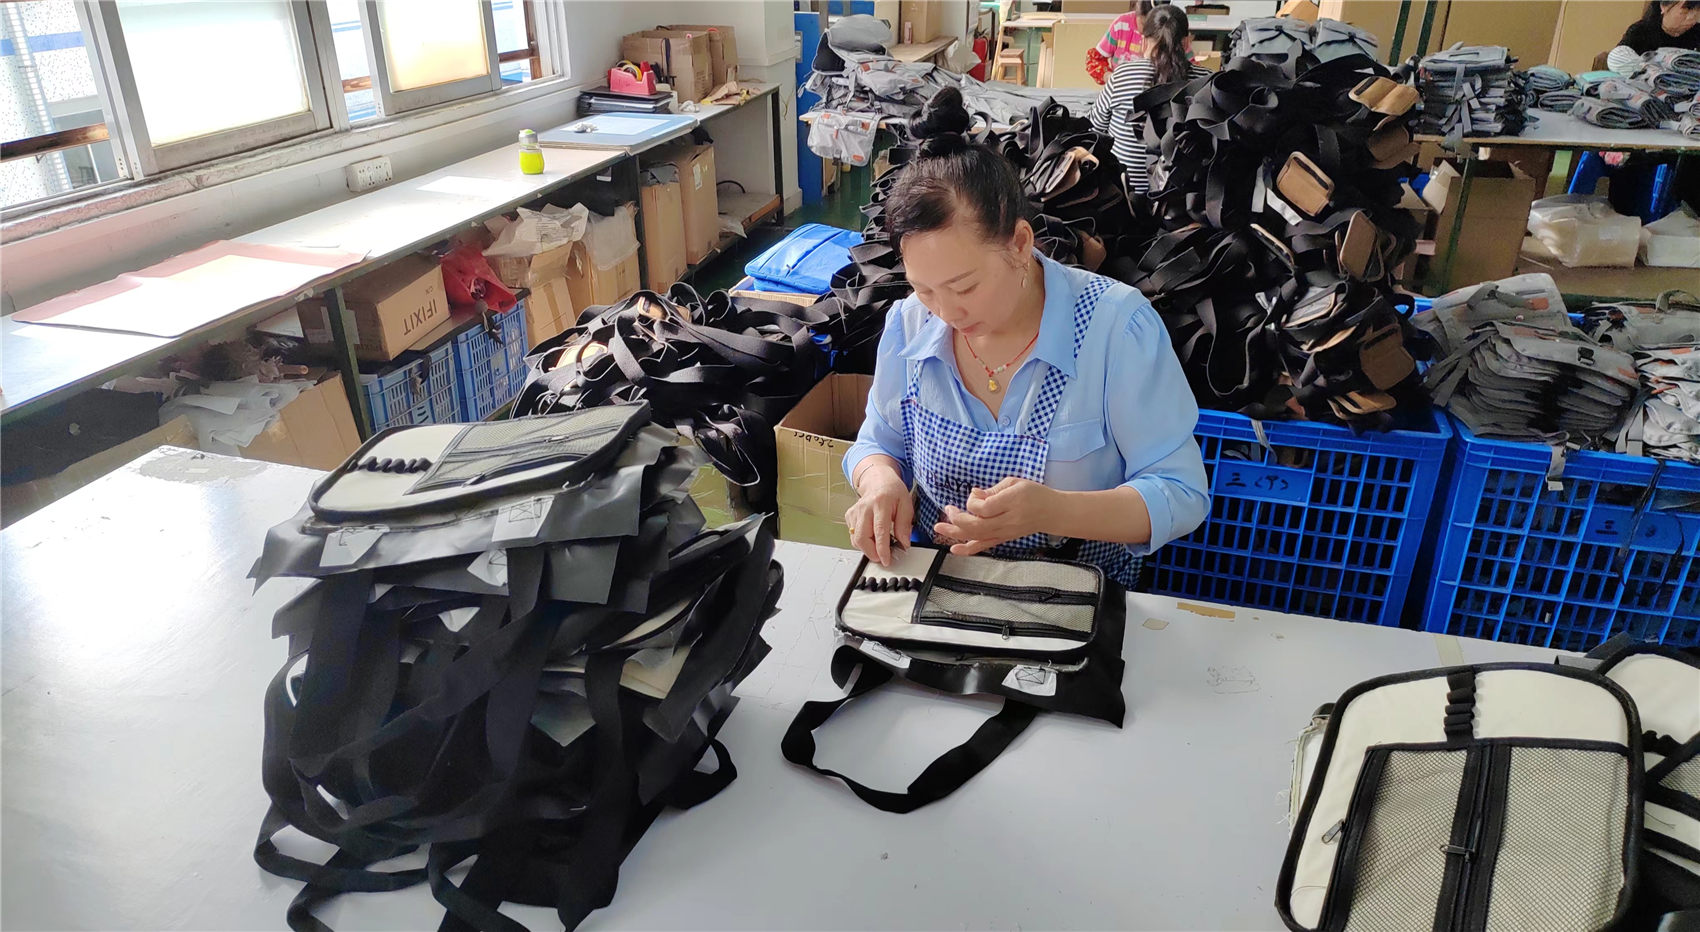
Hebei Ripped Fashion Co., Ltd. was established in 2009 and is located in Baigou Town, Baoding City, Hebei Province—widely known as the “luggage capital of China.” Leveraging its strong local supply chain advantages and mature manufacturing ecosystem, the company has developed into a professional manufacturer specializing in fashion bags and accessories.
Guided by the principles of high-quality products, excellent service, and competitive pricing, Hebei Ripped Fashion Co., Ltd. has built long-term and stable partnerships with overseas retailers, chain stores, and well-known trading companies in China and abroad. Its products are widely distributed across global markets and are well received by customers for their reliability and style.
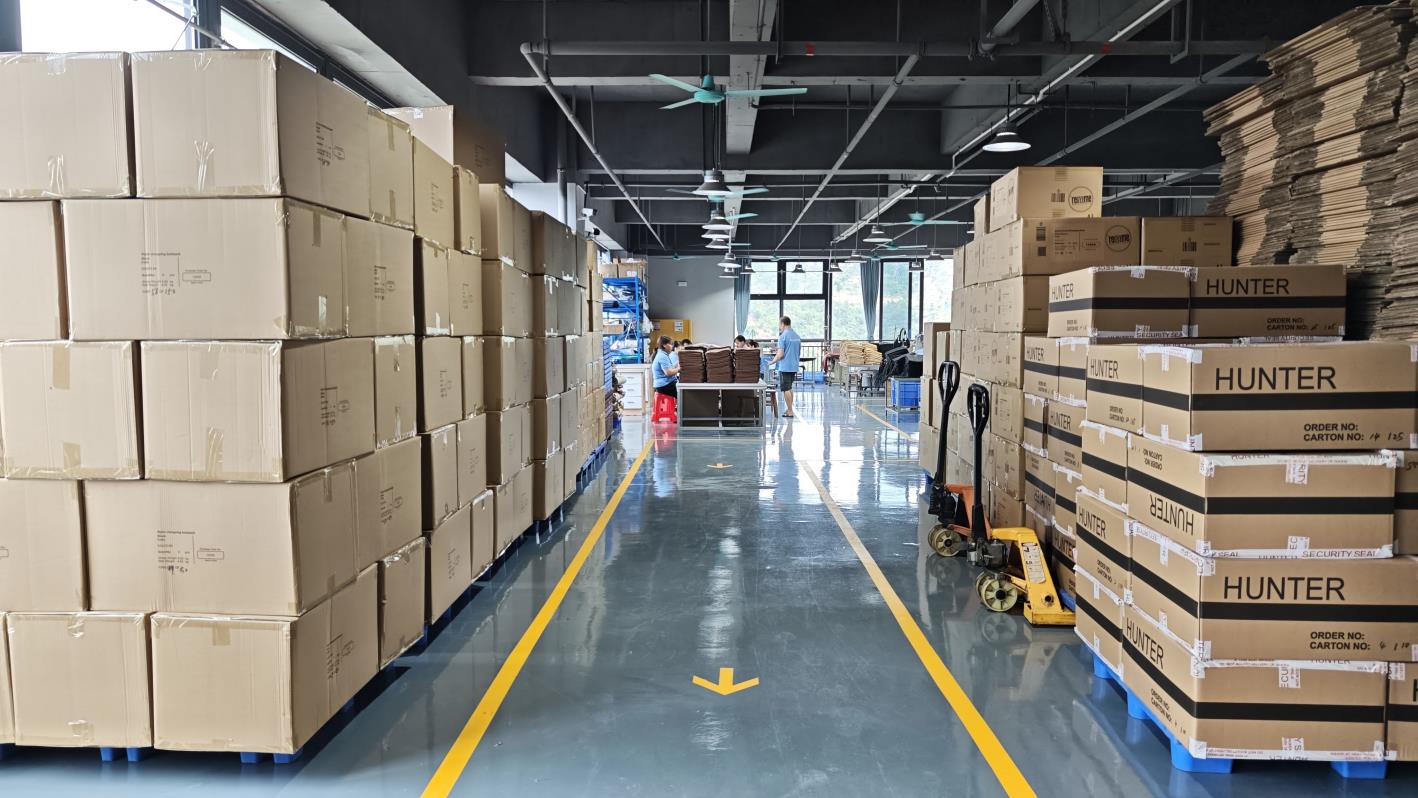
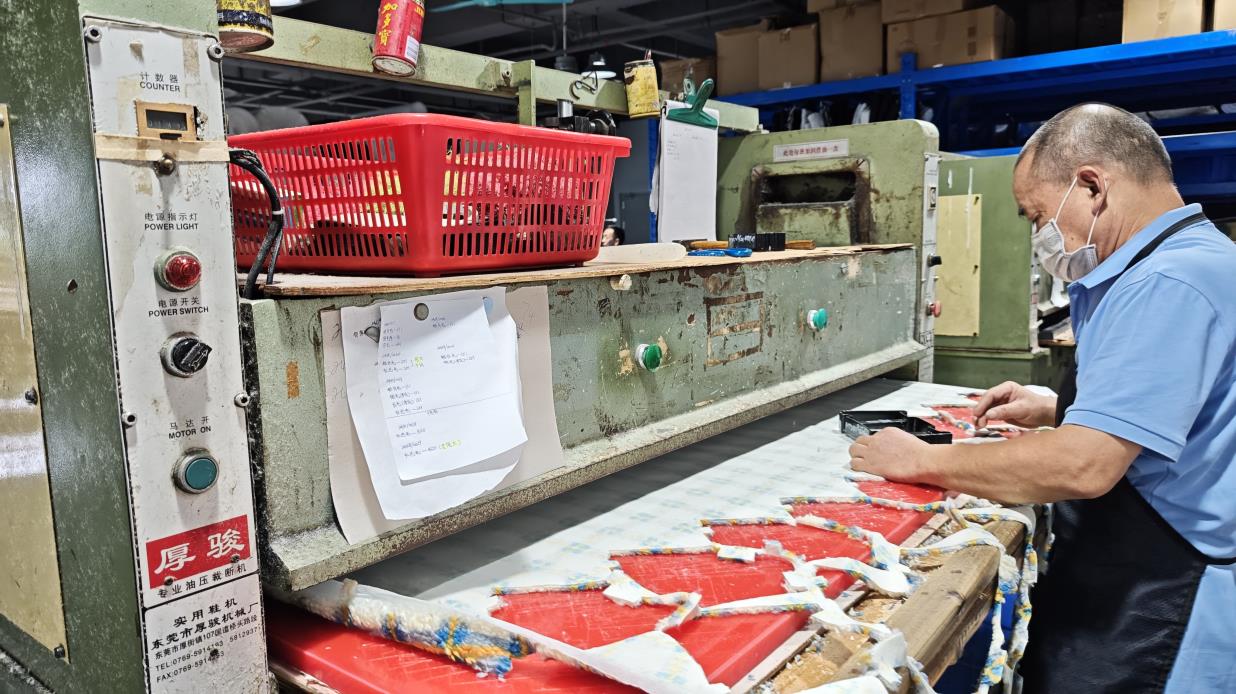
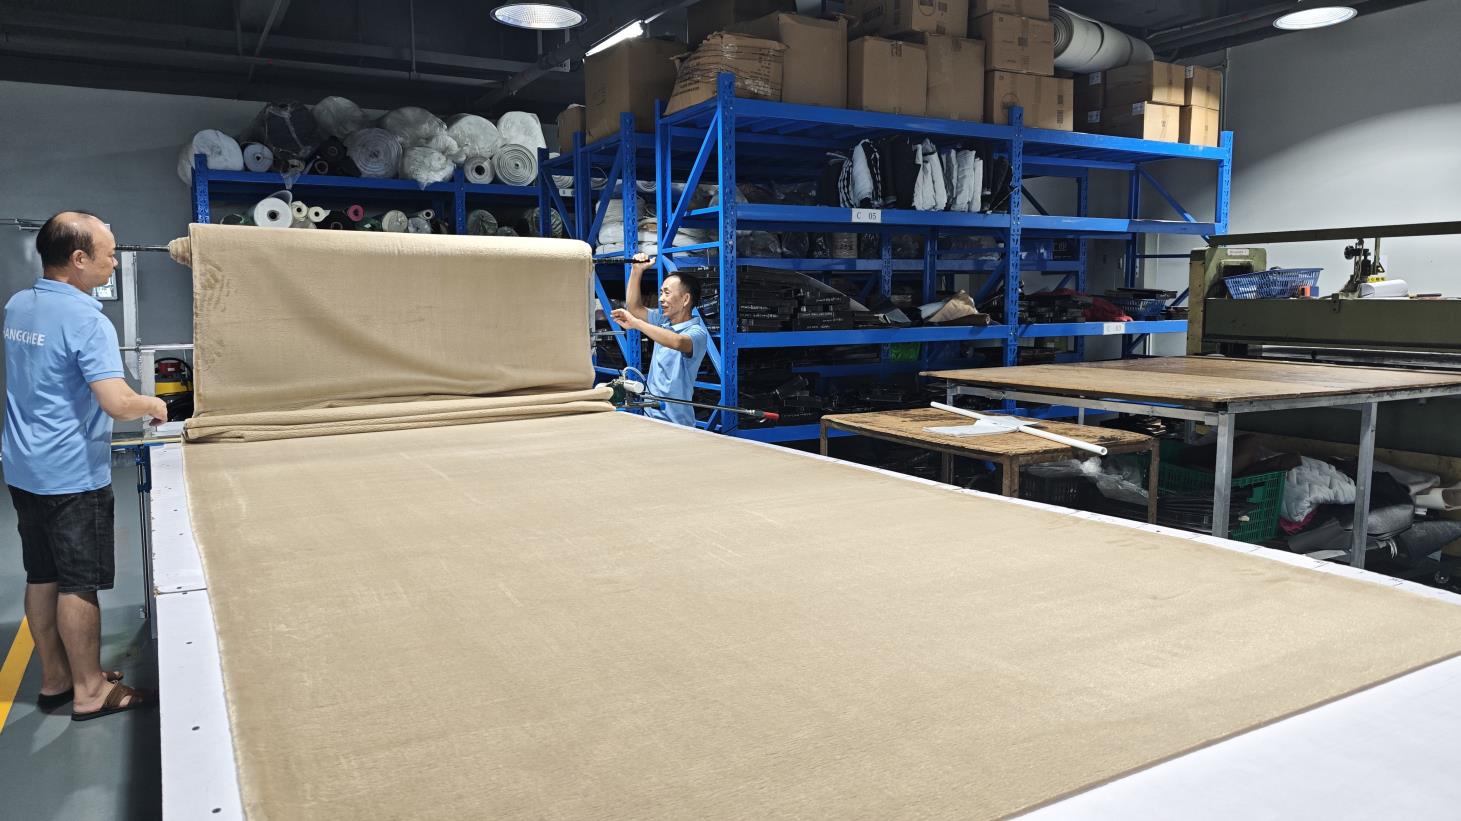
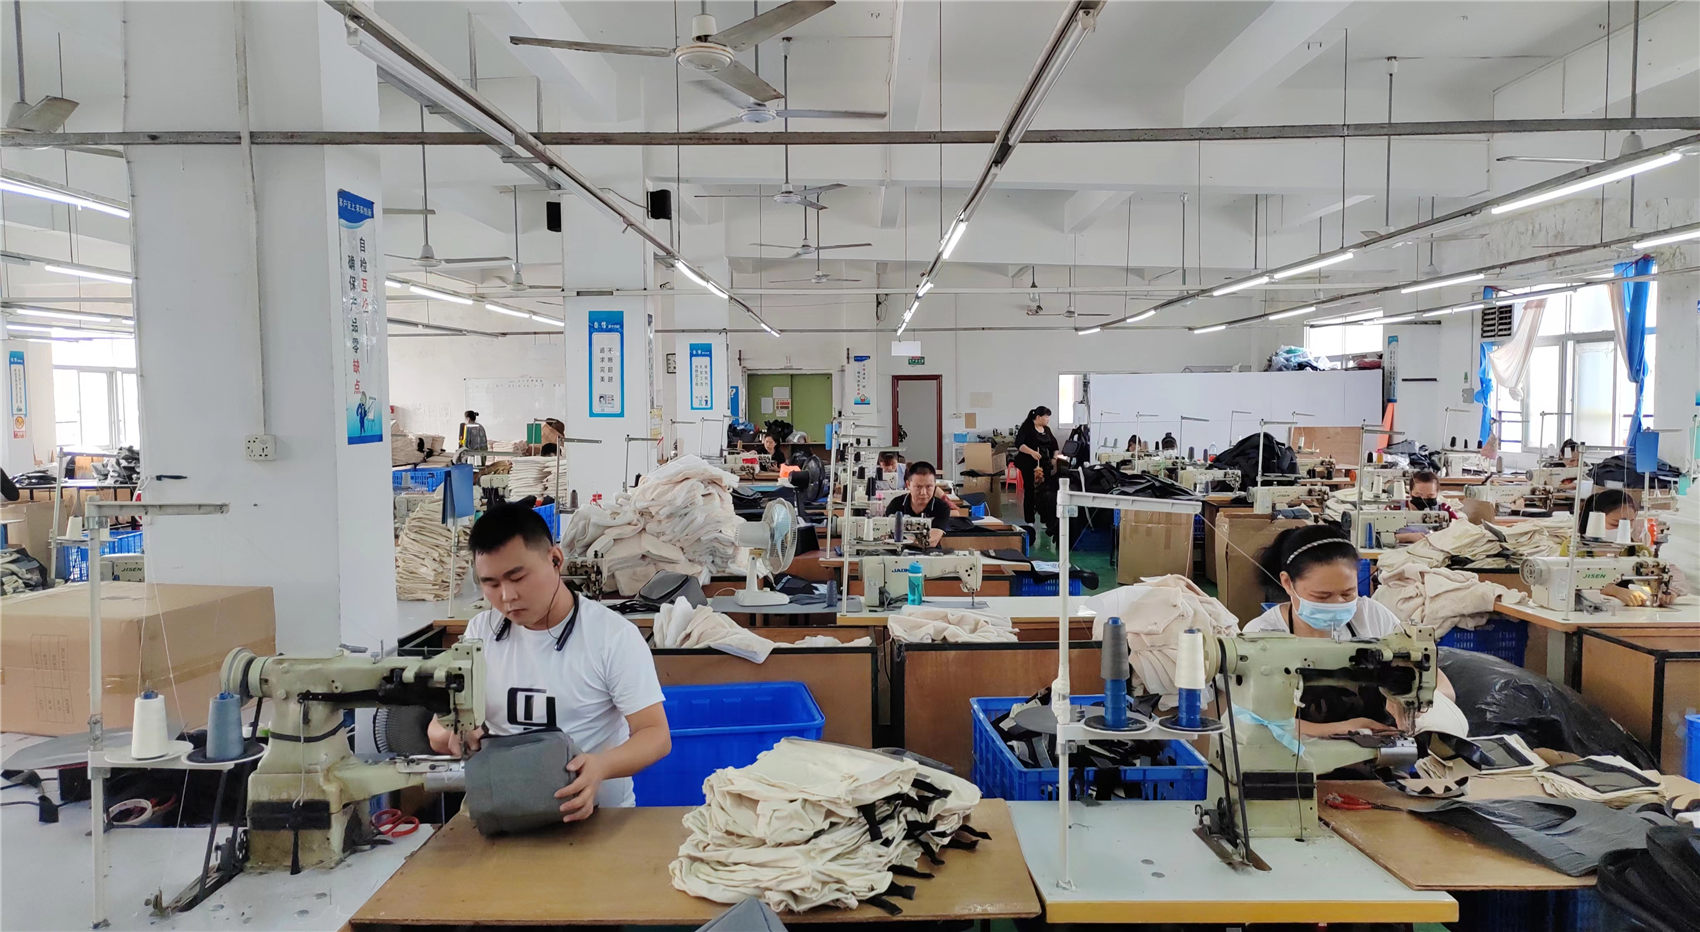
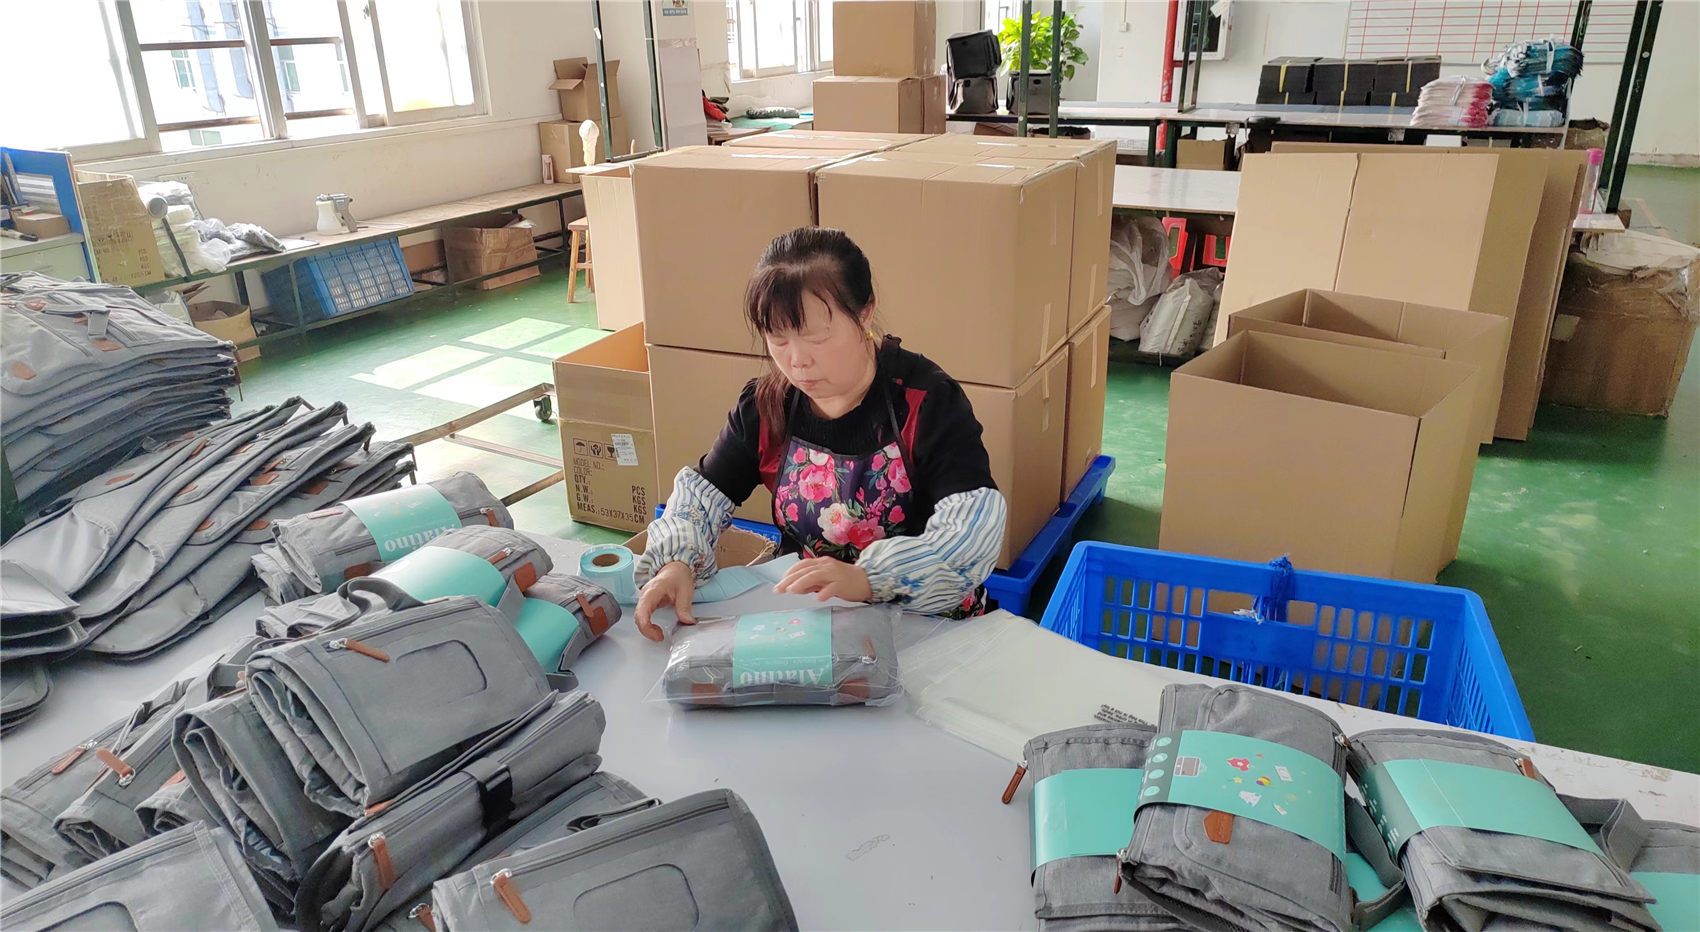
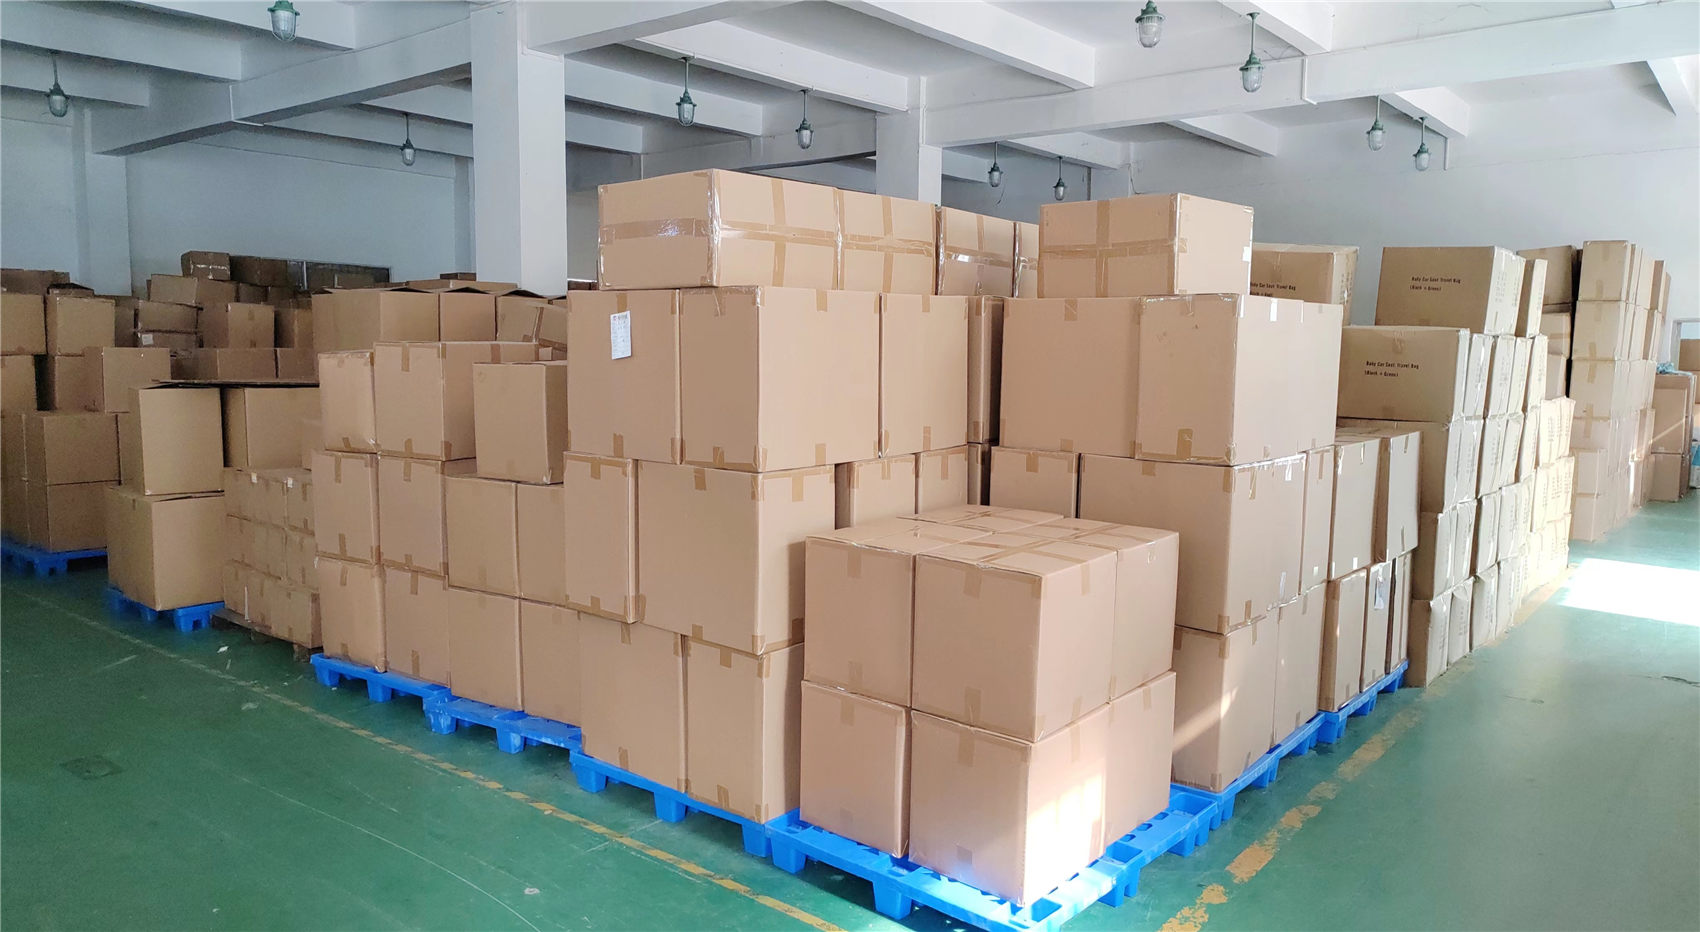
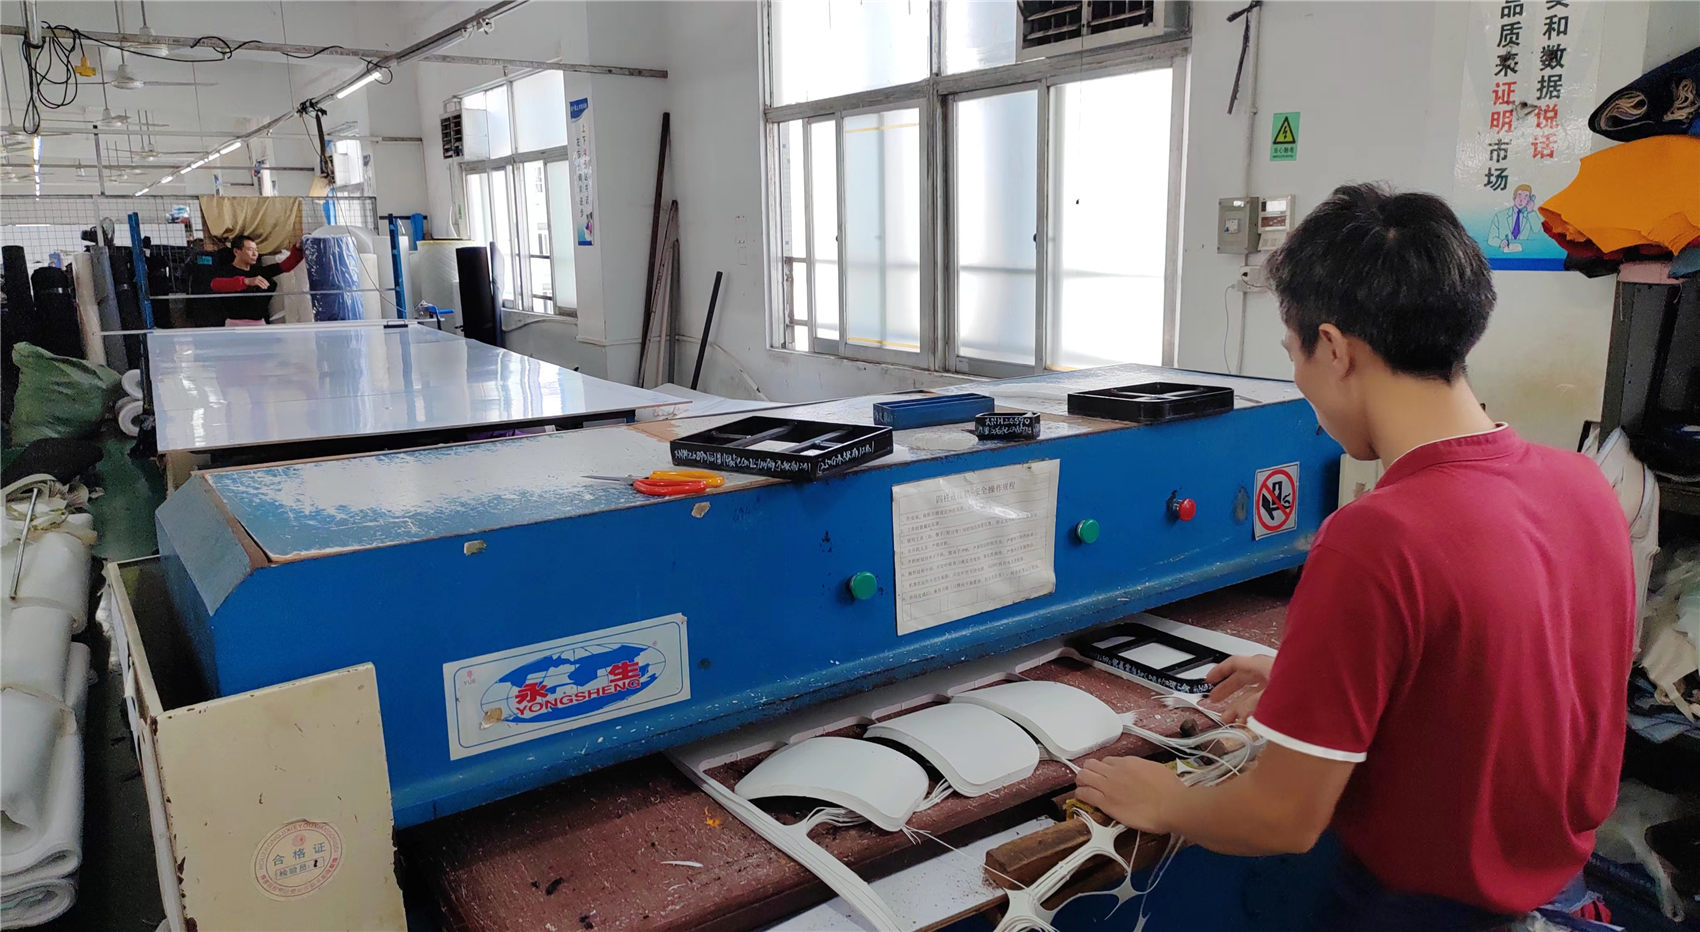
The company occupies a total area of approximately 3,000 square meters, including a 2,000-square-meter production workshop. With a skilled workforce of more than 300 experienced employees, the company maintains strong production capacity and strict quality control throughout the manufacturing process.
Its main product categories include handbags, backpacks, waist bags, tote bags, and shopper bags. The company also provides comprehensive OEM and ODM services, offering flexible customization solutions based on client requirements, including design development, material selection, logo branding, and packaging.
With over 20 years of combined industry experience in bag manufacturing, Hebei Ripped Fashion Co., Ltd. continuously updates its product designs to follow global fashion trends while ensuring durability and practical functionality. Fast delivery, fine craftsmanship, and consistent quality are the company’s core strengths, enabling it to maintain a strong reputation in international markets.
Looking ahead, the company is committed to further expanding its global presence, enhancing product innovation, and delivering more sustainable, stylish, and cost-effective fashion bag solutions to customers worldwide.
Maintaining strict food-contact safety standards and exploring sustainable technical innovations for 2025 and beyond.
Because soft coolers are in constant contact with food, beverages, and medical products, strict adherence to global safety testing parameters is critical. Our manufacturing processes comply with the following standards:
As cooling technologies evolve, our R&D department continues to innovate along three primary pipelines:
Providing clear, expert answers to key purchasing concerns, logistics, and technical specifications.
Browse more durable, fashion-forward backpacks, duffle bags, and tech cases for global sourcing.
 Ripped Fashion